7 Safety Valve Buying Tips for Global Buyers
A safety valve may look like a compact metal fitting, yet its set pressure, capacity, materials, and connection details can affect an entire process. Global buyers therefore need more than a low quote. They need evidence that the selected valve suits the medium, operating conditions, and installation.
Industry reports help explain why careful sourcing matters. Grand View Research’s Industrial Valves Market report identifies oil and gas, power generation, and water and wastewater treatment as important application sectors. These sectors impose very different pressure, temperature, and corrosion demands. The report describes broad market trends, not a substitute for application engineering. That distinction is easy to overlook when comparing suppliers across borders.
Process-safety author Trevor Kletz is often quoted as saying, “If you think safety is expensive, try an accident.” The warning still fits purchasing decisions. A certificate alone cannot prove that a valve will perform as required in a specific system. Buyers should check sizing calculations, material traceability, test records, and the manufacturer’s quality controls. Ask direct questions. Keep the answers on file. A missing detail can become an expensive lesson—and sometimes the paperwork itself needs a second look. These seven buying tips will help global buyers assess suppliers, compare technical offers, and make more defensible decisions.
Define Operating Conditions: Set Pressure, Temperature, Fluid, and Phase
A safety valve should be selected for the conditions it will actually face, not just the equipment’s nameplate pressure. Confirm the protected system’s maximum allowable pressure and the required set pressure with a qualified engineer. Record normal operating pressure too; a valve that operates too close to its set point may simmer or open repeatedly. Small details matter. Include inlet and outlet pressure data, since backpressure can affect capacity and performance.
Temperature changes the choice of body, spring, seals, and trim materials. Document the lowest startup temperature and highest operating or upset temperature, not only the steady-state value. Identify the fluid precisely, including corrosive components, solids, and expected concentration. State whether it is gas, vapor, liquid, or a changing mixture. Two-phase flow can complicate sizing. Do not guess. Use process records and credible engineering calculations, and flag any uncertain values before requesting a quotation.
Tips: Share a simple operating-condition sheet with normal, minimum, and maximum pressure and temperature; fluid composition; phase; and backpressure. Note whether conditions vary during startup, cleaning, or shutdown. It happens: old drawings may not match the current process, so compare them with field measurements and recent operating logs. Ask the supplier to confirm the assumptions used for sizing and material selection.
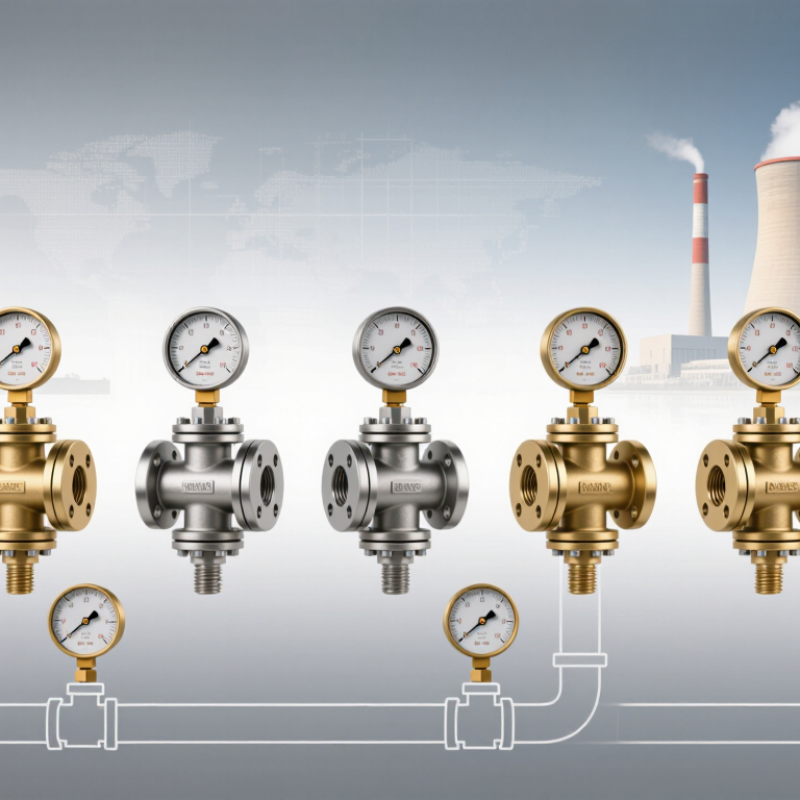
Safety Valve Operating Conditions: Example Pressure Settings
Compare illustrative operating pressures with example valve set pressures. Labels identify the fluid phase and temperature.
These values are illustrative, not design recommendations. Confirm the fluid, phase, temperature, and pressure conditions, and select the set pressure in accordance with the protected equipment’s maximum allowable working pressure (MAWP) and applicable codes.
Size Relief Capacity with API 520 and Check the 10% Overpressure Basis
Relief capacity is not a guess based on pipe size. Use API 520 sizing methods with a defined relieving scenario, required flow rate, fluid properties, temperature, and pressure. Confirm the valve’s set pressure and consider inlet pressure loss and built-up or superimposed backpressure. A small error in any input can change the selected orifice.
The 10% overpressure basis needs careful checking. Overpressure is the pressure rise above the valve’s set pressure, expressed as a percentage of that pressure. Do not assume every valve or service can use a 10% basis. Verify the applicable code, service conditions, valve type, and certified capacity basis before comparing capacity with the required relief load. The allowable pressure accumulation may also depend on the governing design requirements.
A calculation sheet can look precise and still carry a weak assumption. Check units, molecular weight, and the selected discharge coefficient against the relevant documentation. Then have another qualified reviewer trace the inputs back to process data. Small details matter. If the operating case is uncertain, pause and confirm it rather than rounding toward a convenient valve size.
Verify ASME Section VIII Set-Pressure Tolerances: ±2 psi or ±3%
When comparing safety valves, check the set-pressure tolerance in ASME BPVC Section VIII, Division 1, UG-134(d). It specifies ±2 psi for set pressures up to and including 70 psi, and ±3% above 70 psi. These limits are not permission to raise the required set pressure. At 50 psi, the tolerance band is 48–52 psi; at 100 psi, it is 97–103 psi. The distinction is easy to miss when supplier documents mix psi and bar.
Tip: Request the calibrated test record, not only a nameplate photo. Check the set pressure, units, test date, instrument calibration, and applicable code edition. Ask whether the recorded value is the tested opening pressure. Compare it with the vessel’s documented requirement. Keep the records together.
A stamped rating alone is not enough. Verify the serial number and test conditions against the certificate before approval. Low-pressure service deserves extra care because ±2 psi can represent a sizeable share of the set point. Tolerance also does not confirm capacity, materials, or discharge suitability. A tidy document can still contain an error.
Choose Materials and Connections for Corrosion, Service, and Local Standards
A safety valve is only dependable when its wetted materials suit the actual service. Start with the medium, operating temperature, pressure, and likely contaminants—not the product label alone. In a coastal water line, chloride exposure may make standard carbon steel a poor choice. Process fluid can also attack trim, springs, or seals. Check every material, including elastomers. Small details matter.
For hot steam, confirm the valve’s rated temperature and pressure range. Then verify the set pressure and required relieving capacity against the system data. A stainless-steel body does not mean every internal part resists corrosion. Ask for material records and test documentation, and compare them with the project specification. This can feel fussy. It prevents costly mismatches.
Connection choice needs equal care. Match thread type, flange dimensions, pressure class, and facing to the piping and destination standards. Similar-looking threads may not seal together. For export orders, request drawings and certificates that identify the exact standard and revision; “international” is not specific enough. Local approval rules vary by application and country, so have a qualified engineer or inspector confirm them before purchase. I would recheck compatibility even after receiving confirmation, because catalog tables can hide one small mismatch.
Check API 526 Orifice Designations and API 527 Seat-Leakage Test Requirements
An API 526 letter is more than a catalog shortcut. It identifies a standardized orifice area for covered flanged steel pressure-relief valves. Ask the supplier to state the letter, inlet and outlet sizes, set pressure, and certified capacity. Then check capacity against the actual fluid, temperature, and relieving conditions. An orifice letter alone does not prove the valve will pass your required flow. Small details matter.
For seat tightness, request testing to API 527, not a vague “bubble-tight” claim. Leakage limits depend on valve type, test medium, pressure, and the applicable procedure. Ask for the test report to show the medium, test pressure, observed leakage, and acceptance criterion. Compare those details with the purchase specification. Paperwork counts.
A practical review catches mismatches early. The API 526 designation should match the selected valve configuration. The API 527 result should reflect the ordered seat and specified test conditions. One point is easy to miss: a successful workshop test describes controlled conditions, not every field condition. That distinction deserves a second look, even when schedules tighten.